Truck-Lite Europe marks milestone for LED testing facility
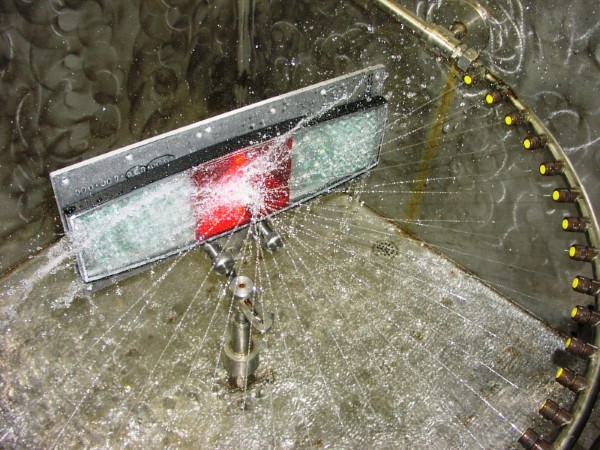
Water resistance testing is among the site’s capabilities
Truck-Lite Europe is marking the first anniversary of its expanded in-house LED lighting testing facility at its Harlow, Essex facility.
The investment in the site provides an additional level of product scrutiny and quality assurance, says Truck-Lite, bringing together a comprehensive range of optical, electronic and environmental testing capabilities. It allows the company to assess lighting performance, durability and regulatory compliance under conditions designed to replicate those encountered in everyday vehicle operation.
Robert Field, validation and legislation manager at Truck-Lite Europe, explained: “Our testing facility provides an additional layer of scrutiny and quality assurance throughout the product validation process. It’s not simply about demonstrating that a lighting system meets the relevant regulations, but also about understanding how it performs when subjected to the environmental and operational stresses experienced by commercial vehicles.
“By carrying out these demanding tests in-house, we can identify potential weaknesses, verify product performance and maintain greater control over quality. Ultimately, this provides our OEM customers, vehicle converters and fleet operators with further reassurance that the lighting systems they specify are designed and tested for long-term reliability.”
Among the facility’s key capabilities is a 2,000-hour static LED endurance test, which subjects products to repeated power switching and thermal cycling between +23°C and +60°C. This process assesses electronic and thermal stability over prolonged operating periods.
Environmental testing includes a 96-hour chamber cycle, exposing products to temperatures ranging from –40°C to +60°C and relative humidity levels of up to 95 per cent. Testing can also incorporate vibration to evaluate the combined effects of temperature, moisture and mechanical stress.
Water resistance is assessed through IPX4 spray testing, using 30 rotating water jets and full 360-degree product rotation during one hour of continuous exposure.
The facility also incorporates an optical testing tunnel and reflex testing area, enabling precise measurement of light output, colour accuracy and reflectivity against relevant UN ECE regulatory requirements.
Together, says Truck-Lite, these processes support the validation of printed circuit board assemblies (PCBAs), LED performance and complete lighting systems, while providing valuable data for ongoing product development and quality control.
Truck-Lite Europe supplies a variety of CV lighting products, wiring harnesses, reflectors and associated equipment.